Die Casting Manufacturing Equipment: Explore Machines and Production Processes
Metal components used in automotive systems, industrial machinery, electronics, and consumer equipment often require precise shapes and consistent dimensions.
Die casting manufacturing equipment makes this possible by injecting molten metal into specially designed steel molds under controlled pressure, allowing manufacturers to produce complex components repeatedly.
Modern die casting operations combine high-pressure injection machines, precision dies, metal melting systems, temperature controls, and automated handling equipment. Each part of the production line contributes to the quality, dimensional accuracy, and repeatability of the finished component.
Understanding how these machines work helps explain the complete manufacturing process, from preparing molten metal to inspecting finished castings. It also reveals how equipment selection, mold design, process monitoring, and finishing operations influence production performance.
How Die Casting Equipment Forms Metal Components
Die casting uses pressure to force molten metal into a reusable metal mold, commonly called a die. The metal fills the mold cavity, takes its shape, and solidifies before the machine opens and releases the component.
Unlike processes that rely primarily on gravity to fill a mold, pressure-driven die casting can fill intricate cavities quickly. This makes it suitable for producing components with thin walls, detailed features, and repeatable dimensions.
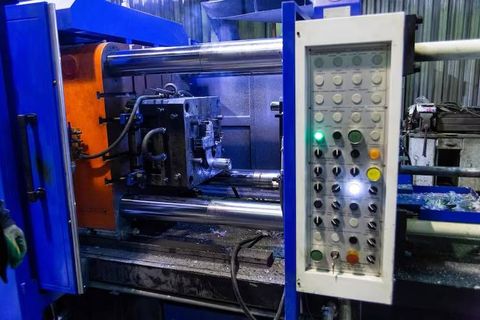
The main equipment includes a casting machine, a die assembly, a metal melting and delivery system, temperature-control equipment, and supporting automation. The configuration depends on the metal being processed, component geometry, production volume, and required quality standards.
Die casting is commonly associated with aluminum, zinc, and magnesium alloys. Each material has different melting characteristics, flow behavior, and solidification requirements, so the equipment and process settings must match the selected alloy.
Hot-Chamber and Cold-Chamber Casting Machines
The two principal machine configurations are hot-chamber and cold-chamber die casting. Their main difference is how molten metal reaches the injection system.
Hot-Chamber Die Casting
In a hot-chamber machine, the injection mechanism is immersed in or directly connected to the molten metal supply. A piston forces metal through a passage and into the die cavity.
This arrangement supports rapid production because the metal delivery system remains integrated with the melting unit. It is commonly used for suitable zinc alloys and other low-melting-point materials compatible with the machine's components.
The main limitation is material compatibility. The immersed injection components must withstand prolonged contact with the molten alloy, making this configuration unsuitable for many higher-temperature aluminum and magnesium casting applications.
Cold-Chamber Die Casting
Cold-chamber machines use a separate melting furnace. For each cycle, a measured quantity of molten metal is transferred into a shot sleeve, where an injection piston pushes it into the die.
This arrangement is widely used for aluminum alloys and is also suitable for other alloys requiring this configuration. Separating the injection mechanism from the main molten-metal reservoir helps accommodate higher processing temperatures.
Cold-chamber machines require careful coordination between metal transfer, injection timing, and temperature control. Delays or inconsistent metal preparation can affect filling behavior and casting quality.
The Main Equipment Used in a Die Casting Line
A die casting operation involves several interconnected machines and supporting systems. The casting press is central to the process, but it cannot operate effectively without suitable tooling, metal preparation, and process controls.
Die Casting Machine and Clamping System
The casting machine provides the force needed to close the die and maintain closure during injection. Its clamping system must resist the force generated as molten metal enters the cavity under pressure.
Machine capacity is selected according to factors such as projected casting area, injection pressure, component dimensions, and die requirements. Insufficient clamping capacity can allow the mold to separate slightly, producing flash or other defects.
Hydraulic systems are commonly used to generate clamping and injection forces, although machine designs vary. Modern equipment may incorporate programmable controls that coordinate machine movement, injection stages, pressure, and cycle timing.
Dies, Cores, and Ejection Systems
The die determines the shape of the casting. It typically consists of two principal halves mounted on the machine, with internal cavities and features designed around the component's geometry.
Movable cores or slides can create openings, recesses, and undercuts that cannot be formed by a simple two-part mold. These mechanisms increase design flexibility but also introduce additional tooling and maintenance requirements.
After the metal solidifies sufficiently, the machine opens the die and ejector pins push the casting out. Ejection must be carefully designed to prevent deformation, surface damage, or sticking inside the mold.
Melting Furnaces and Metal Delivery Systems
Melting equipment brings the selected alloy to the required temperature and helps maintain suitable conditions throughout production. Depending on the installation, holding furnaces may keep molten metal available near the casting machine.
Metal transfer systems, ladles, and automated dosing equipment deliver controlled quantities into the injection system. Consistent dosing reduces variation between cycles and supports stable mold filling.
Molten-metal handling also requires appropriate temperature monitoring, protective equipment, and procedures for controlling contamination. Moisture must be kept away from molten metal because it can create serious safety hazards.
How a Typical Die Casting Production Cycle Works
Although machine designs differ, a conventional production cycle follows a coordinated sequence.
First, the operator or automated system confirms that the die is correctly installed, closed, and prepared for casting. Lubrication or release agents may be applied where required to support metal flow and facilitate ejection.
Next, molten metal is delivered to the injection system. The machine drives the metal into the die cavity, using controlled injection speed and pressure to fill the mold and pack the metal as it solidifies.
Cooling follows injection. The die extracts heat from the metal, allowing the component to develop sufficient strength for removal. The required cooling time depends on the alloy, casting thickness, die temperature, and production conditions.
The die then opens, ejector mechanisms release the component, and the cycle begins again. Excess material, such as runners, gates, and overflow sections, may be separated during subsequent operations.
Because the process repeats many times, small variations in temperature, injection timing, or die condition can affect a large number of components. Stable process control is therefore essential for consistent production.
Temperature Control and Process Monitoring
Temperature management influences nearly every stage of die casting. Molten metal must remain within an appropriate processing range, while the die needs to maintain conditions that support reliable filling and solidification.
Die temperature-control systems may use cooling channels, water circuits, or other controlled thermal-management arrangements. Some dies also require localized heating to maintain suitable conditions in specific areas.
Injection parameters matter just as much. Metal velocity, pressure, filling time, and the transition between injection stages influence how the cavity fills and how trapped air or gases behave.
Modern control systems can record process parameters and flag deviations from established operating limits. Monitoring does not eliminate defects, but it helps operators identify changing conditions before they create extensive production problems.
Common Casting Defects and Their Causes
Even well-equipped facilities can experience defects if material preparation, tooling, or machine settings are not properly controlled.
Porosity occurs when gas or shrinkage-related voids form inside the casting. Its causes may include trapped air, inadequate venting, contamination, or unsuitable solidification conditions.
Cold shuts and misruns occur when metal fronts fail to join properly or the cavity does not fill completely. Low metal temperature, poor flow conditions, or insufficient injection performance may contribute.
Flash is excess thin metal that escapes between die surfaces. It can indicate problems involving die alignment, clamping force, tooling wear, or process settings.
Dimensional variation may result from inconsistent temperatures, die wear, uneven cooling, or unstable operating conditions.
Manufacturers address these problems through systematic inspection, process adjustments, tooling maintenance, and defect analysis rather than relying on visual checks alone.
Finishing, Inspection, and Automation
Freshly cast components often require additional processing before they are ready for assembly or use. Trimming presses remove runners and excess metal, while machining equipment creates precise holes, threads, or mating surfaces when the casting process alone cannot achieve the required tolerances.
Surface finishing may include deburring, blasting, polishing, or other treatments appropriate to the application. Some components also receive coatings or protective finishes.
Inspection methods depend on the component's function. Dimensional measurement, visual inspection, leak testing, and mechanical testing may be used to verify requirements. X-ray inspection can help identify internal porosity or other hidden discontinuities when the application justifies it.
Automation connects these stages through robotic metal handling, part extraction, trimming, conveyor systems, and inspection equipment. Properly integrated automation can improve repeatability and reduce direct handling, although it requires careful coordination and maintenance.
Frequently Asked Questions
What metals are commonly used in die casting?
Aluminum, zinc, and magnesium alloys are common choices. The appropriate material depends on the component's strength, weight, corrosion resistance, geometry, and operating environment.
What is the difference between hot-chamber and cold-chamber die casting?
Hot-chamber machines keep the injection mechanism integrated with the molten-metal supply. Cold-chamber machines transfer molten metal into a separate injection sleeve for each cycle.
Why is die design important in manufacturing?
Die design controls the component's geometry, metal flow, cooling behavior, and ejection. A well-designed die helps maintain dimensional consistency and reduces the risk of defects.
Can die casting produce complex components?
Yes. Die casting can produce detailed shapes, thin walls, and integrated features. However, achievable complexity depends on the alloy, machine capability, die design, and required component quality.
How do manufacturers maintain consistent casting quality?
They control metal and die temperatures, injection parameters, tooling condition, and material preparation. Inspection and process monitoring help identify defects and production variation.
Conclusion
Die casting manufacturing equipment combines precision machinery, reusable steel dies, molten-metal handling systems, and process controls to produce consistent metal components. Each stage, from injection and cooling to finishing and inspection, contributes to the final part's performance.
Reliable production depends on matching the machine configuration to the alloy and component requirements. With suitable tooling, stable process conditions, and effective quality control, manufacturers can produce complex castings while maintaining repeatability across high-volume production runs.
Related Post...
EPS Recycling Machines and Foam Recycling Systems: Explore Recycling Basics
Updated: September 08, 2026
Read More
Fluid Pump Systems Discover How Modern Industries Improve Flow Efficiency
Updated: July 22, 2026
Read More
High-Speed Rotary Tablet Press Machines: Explore Tablet Compression Processes
Updated: October 02, 2026
Read More