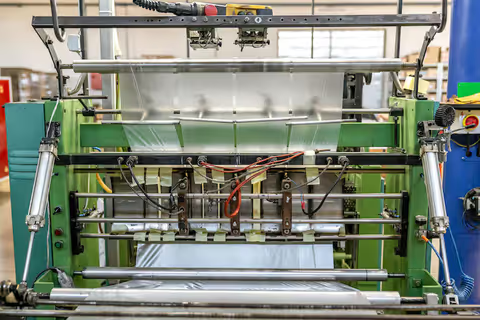
Plastic Extrusion Machines: Learn About Types, Functions and Industrial Uses
Plastic extrusion machines are industrial systems used to transform plastic materials into continuous products with a consistent cross-sectional shape. They are widely used for producing pipes, sheets, films, profiles, tubing, insulation layers, and other plastic products.
A plastic extrusion machine generally works by feeding polymer material into a heated barrel, melting it, pushing it through a shaped die, and cooling the resulting product. Understanding how these machines operate helps explain how many common plastic products are manufactured.
Context
What Are Plastic Extrusion Machines?
Plastic extrusion machines are production systems designed to process polymer materials continuously. Unlike processes that create individual molded pieces, extrusion produces a long, continuous output that can later be cut, wound, or processed into specific lengths.
The basic system contains a material feed section, screw mechanism, heated barrel, die, cooling equipment, and take-up or cutting equipment. Each part has a specific role in controlling the movement and transformation of the polymer.
The extrusion concept developed alongside advances in polymer processing and mechanical engineering. Early systems were relatively simple, while modern equipment incorporates temperature sensors, motor controls, pressure monitoring, automated adjustments, and digital data collection.
How Does Plastic Extrusion Work?
The process begins when plastic pellets, granules, powder, or other prepared feedstock enter the hopper. A rotating screw then moves the material through a heated barrel.
As the material travels through the barrel, heat and mechanical energy gradually soften or melt the polymer. The screw also helps mix the material and maintain a controlled flow toward the die.
At the end of the barrel, the molten polymer passes through the die opening. The die determines the basic shape of the emerging material. Cooling equipment then reduces the temperature so that the product retains its intended dimensions.
Typical stages include:
- Material feeding
- Conveying and melting
- Mixing and homogenization
- Pressure development
- Die forming
- Cooling or solidification
- Dimension control
- Cutting or winding
Main Types of Plastic Extrusion Machines
Different extrusion machines are designed around the material, product geometry, and processing requirements. Single-screw extruders use one rotating screw and are widely used for many standard polymer-processing applications.
Twin-screw extruders use two screws that operate within the same barrel. Depending on the screw arrangement, they can provide enhanced mixing and are commonly associated with compounding, filled polymers, and materials containing multiple components.
Film extrusion systems produce thin plastic films. Blown-film systems form a tubular film that is expanded with air, while cast-film systems spread molten polymer through a flat die before cooling it on a chilled surface.
Sheet extrusion systems produce wider and thicker flat materials. Profile extrusion is used for continuous shapes such as channels, strips, seals, and architectural profiles.
| Extrusion Type | Typical Output | Main Process Characteristic |
|---|---|---|
| Single-screw | Pipes, sheets, profiles | Straightforward continuous processing |
| Twin-screw | Compounded polymers | Intensive mixing and material preparation |
| Blown film | Flexible films | Tubular film formation |
| Cast film | Flat films | Flat-die extrusion and rapid cooling |
| Sheet extrusion | Plastic sheets | Wide flat output |
| Profile extrusion | Continuous profiles | Shaped die geometry |
Importance
Why Plastic Extrusion Machines Matter
Plastic extrusion is important because it provides a continuous method for producing products with controlled dimensions. Many industries depend on continuous plastic components for construction, electrical systems, packaging, transportation, agriculture, consumer products, and industrial equipment.
The process can accommodate a broad range of polymers and product shapes. By changing the screw configuration, die, temperature conditions, cooling method, and line speed, manufacturers can process materials for different applications.
For everyday users, extrusion technology is present in products that may not immediately appear to involve polymer processing. Plastic pipes, electrical insulation, window profiles, protective films, sheets, and flexible tubing can all involve extrusion-based production.
Factors That Influence Product Quality
Extrusion quality depends on several connected variables. Temperature must remain within a suitable processing range for the selected polymer. Excessive heat can cause material degradation, while insufficient heat can make melting and flow difficult.
Screw speed influences material movement, mixing, pressure, and output rate. Die design affects the shape and dimensions of the product, while cooling conditions influence shrinkage and final geometry.
Other important factors include:
- Polymer moisture content
- Feed consistency
- Melt temperature
- Screw configuration
- Die pressure
- Cooling rate
- Puller speed
- Product thickness
- Environmental conditions
Maintaining consistent relationships among these variables is important because a change in one part of the process can affect other stages.
Materials Used in Extrusion
Plastic extrusion machines can process thermoplastics with different physical and thermal characteristics. Common materials include polyethylene, polypropylene, polyvinyl chloride, polystyrene, polyethylene terephthalate, and various engineering polymers.
Material selection depends on the required strength, flexibility, temperature resistance, chemical resistance, transparency, electrical properties, and intended application. Additives, fillers, pigments, stabilizers, and recycled polymer content can also change processing behavior.
Recent Updates
Automation and Digital Monitoring
Modern extrusion lines increasingly use digital control systems to monitor temperature, pressure, screw speed, motor load, and line speed. Operators can view process information through electronic control panels rather than relying entirely on manual readings.
Automated control can also coordinate several parts of an extrusion line. For example, the screw, cooling system, haul-off equipment, and winding unit can operate according to linked process parameters.
Improved Thickness and Dimension Control
Thickness control has become an important area of development, particularly for films and sheets. Sensors can measure dimensions during production, allowing control systems to detect variations and adjust selected process parameters.
Laser-based measurement, optical sensors, machine vision, and other monitoring technologies can be integrated into some production environments. These systems help generate process data for quality analysis.
Energy and Material Efficiency
Energy management has become increasingly relevant as manufacturers examine electricity use across heating, motors, cooling, and auxiliary equipment. Modern systems may use improved heating controls, variable-speed drives, insulation, and automated temperature management.
Material efficiency is also receiving attention. Process monitoring can help identify unstable conditions that may generate excessive scrap. Recycled polymers and production regrind are also being incorporated into some extrusion applications when their material characteristics are suitable.
Advanced Process Analysis
Computer-based simulation can be used to examine polymer flow through screws and dies before physical production begins. Such analysis can help engineers study pressure distribution, temperature behavior, residence time, and potential flow problems.
Cybersecurity is another consideration as extrusion equipment becomes connected to factory networks. Access controls, network segmentation, software management, and secure data handling can become part of industrial equipment planning.
Laws or Policies
Indian Regulatory Framework
In India, plastic extrusion activities can be affected by environmental, workplace safety, product-specific, and waste-management requirements. The applicable rules depend on the type of plastic product, manufacturing activity, facility location, and material used.
The Environment (Protection) Act, 1986 provides a broad legal framework for environmental protection. Pollution-related requirements may involve the Central Pollution Control Board (CPCB) and the relevant State Pollution Control Board.
The Plastic Waste Management Rules, 2016, together with subsequent amendments and related requirements, address aspects of plastic waste management and producer responsibilities. Extended Producer Responsibility provisions can apply to specified plastic packaging categories.
Workplace safety is also relevant to extrusion plants because equipment can involve high temperatures, rotating machinery, electrical systems, pressure, and moving material. Applicable occupational safety requirements should be reviewed according to the facility and jurisdiction.
Standards and Technical Guidance
Bureau of Indian Standards publications may be relevant to particular plastic products, materials, testing procedures, or dimensions. International standards from organizations such as ISO and IEC may also be used for product testing, equipment safety, electrical systems, and quality management.
Regulatory requirements can vary according to the product and application. Therefore, manufacturers and facility operators need to identify the rules applicable to their specific operation rather than relying on a single general requirement.
Tools and Resources
Process Monitoring Tools
Several tools are used to understand and control extrusion processes. Temperature controllers and thermocouples monitor heating zones, while pressure sensors provide information about melt pressure near important process locations.
Dimensional gauges, laser measurement systems, optical sensors, and weighing equipment can help evaluate product geometry and material output. Data-logging systems can record process variables for later analysis.
Design and Calculation Resources
Extrusion calculations may involve screw speed, throughput, residence time, die dimensions, cooling conditions, and material density. Engineering software and polymer-processing calculators can assist with preliminary analysis.
Manufacturers and engineers may also use die-design references, polymer datasheets, technical manuals, ISO publications, BIS resources, and CPCB guidance documents. These resources provide information that can help explain material behavior, product requirements, and regulatory considerations.
Typical Resources for Learners
People learning about plastic extrusion can examine:
- Polymer material datasheets
- Extrusion machine manuals
- Die-design references
- BIS standards and publications
- CPCB environmental guidance
- ISO technical standards
- Industrial process-control documentation
- Polymer-processing textbooks
- Computer-based extrusion simulation tools
The appropriate resource depends on whether the reader is studying materials, machine operation, product design, quality control, or environmental requirements.
FAQs
What Are Plastic Extrusion Machines Used For?
Plastic extrusion machines are used to produce continuous plastic products such as pipes, films, sheets, tubing, profiles, insulation layers, and other shaped materials. The die determines the basic cross-sectional form of the output.
How Does a Plastic Extrusion Machine Work?
A plastic extrusion machine feeds polymer material into a heated barrel. A rotating screw moves and melts the material before pushing it through a die, after which the shaped output is cooled and controlled.
What Materials Can Plastic Extrusion Machines Process?
Many thermoplastic materials can be processed through extrusion. Examples include polyethylene, polypropylene, PVC, polystyrene, PET, and selected engineering polymers. Processing conditions vary according to the characteristics of each material.
What Is the Difference Between Single-Screw and Twin-Screw Extrusion?
A single-screw machine uses one rotating screw and is suitable for many continuous extrusion applications. A twin-screw machine uses two screws and can provide enhanced mixing, making it useful for compounding and processing formulations with multiple components.
What Factors Affect Plastic Extrusion Quality?
Important factors include material preparation, moisture, melt temperature, screw speed, pressure, die design, cooling rate, and line speed. Consistent control of these variables helps maintain product dimensions and material properties.
Conclusion
Plastic extrusion machines transform polymer materials into continuous products through controlled feeding, melting, shaping, and cooling. Different machine configurations support applications ranging from films and sheets to pipes, profiles, and tubing. Recent developments emphasize digital monitoring, automated process control, dimensional measurement, material efficiency, and energy management. In India, environmental, waste-management, workplace safety, and product-specific requirements can all influence how extrusion operations are planned and managed.
Related Post...
Laser-Assisted Machining: Exploring Methods, Materials and Machining Techniques
Updated: September 10, 2026
Read More
Polishing Machine: Complete Guide, Basics, and Detailed Explanation
Updated: August 22, 2026
Read More
Plastic Compression Molding Machine Guide for Modern Manufacturing Processes
Updated: September 07, 2026
Read More