Industrial Vacuum Pumps: Types, Working, Applications & Selection
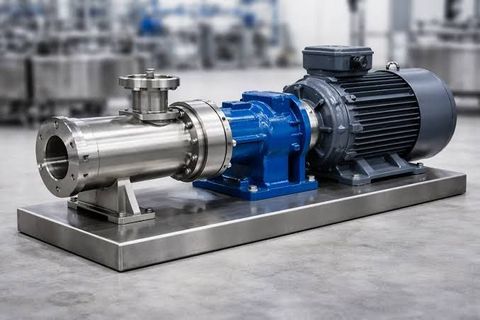
Industrial vacuum pumps are mechanical systems designed to remove gases and air from a sealed chamber or process system to create and maintain a vacuum.
They are used across manufacturing, chemical processing, food processing, pharmaceuticals, electronics, packaging, and other industrial applications.
Different vacuum pump technologies are designed for different pressure ranges, gas compositions, flow requirements, and operating conditions. Selecting the appropriate pump requires an understanding of the process and the level of vacuum required.
What Are Industrial Vacuum Pumps?
Industrial vacuum pumps create a pressure below atmospheric pressure by extracting gas molecules from a closed system. Depending on the technology, the pump may use mechanical displacement, liquid sealing, dry compression, or other operating principles.
A vacuum pump system typically includes:
- Vacuum pump
- Inlet and outlet connections
- Valves
- Filters
- Vacuum gauges
- Piping
- Control systems
- Cooling arrangements
- Separators or condensers where required
The complete system is generally designed around the required vacuum level, pumping speed, gas composition, and process conditions.
Types of Industrial Vacuum Pumps
Rotary Vane Vacuum Pumps
Rotary vane pumps use rotating vanes inside an eccentric chamber to trap and compress gas. Oil-sealed designs are commonly used where relatively clean gases and reliable vacuum generation are required.
They can be used in packaging, laboratory equipment, material handling, and industrial processing.
Liquid Ring Vacuum Pumps
Liquid ring pumps use a rotating impeller and a sealing liquid to compress gases. Water is commonly used as the operating liquid.
These pumps can be suitable for applications involving wet gases, vapors, and processes where contamination resistance is important.
Dry Vacuum Pumps
Dry vacuum pumps operate without oil or another sealing liquid in the pumping chamber. Depending on the design, they may use screws, claws, scrolls, or other mechanisms.
They are used in processes where oil contamination needs to be minimized.
Screw Vacuum Pumps
Screw vacuum pumps use synchronized rotating screws to transport and compress gases. They can provide continuous operation and are used in industrial processes requiring relatively high pumping capacity.
Piston Vacuum Pumps
Piston pumps use reciprocating pistons to remove and compress gases. Their configuration can be suitable for specific industrial applications requiring mechanical displacement.
How Industrial Vacuum Pumps Work
Although operating principles vary, the basic process involves removing gas from a system until the desired pressure is reached.
1. Gas Entry
Gas enters the pump through the inlet connection from the process chamber or vacuum system.
2. Gas Trapping
The pump mechanism captures a specific volume of gas using rotating, reciprocating, or other mechanical components.
3. Compression
The trapped gas is compressed as the pumping mechanism moves through its operating cycle.
4. Gas Discharge
Compressed gas leaves the pump through the exhaust outlet.
5. Pressure Control
Sensors and control equipment can monitor system pressure and regulate operation according to process requirements.
Main Components
| Component | Function |
|---|---|
| Pumping mechanism | Removes and compresses gas |
| Motor | Provides mechanical power |
| Inlet port | Connects to vacuum system |
| Exhaust port | Discharges compressed gas |
| Seals | Reduce unwanted gas leakage |
| Bearings | Support rotating components |
| Vacuum gauge | Measures system pressure |
| Valves | Control gas flow |
| Filter | Protects pump from contaminants |
| Cooling system | Controls operating temperature |
The exact components vary according to pump technology and application.
Applications of Industrial Vacuum Pumps
Food Processing and Packaging
Vacuum pumps are used in vacuum packaging, product handling, drying, freeze-drying, and other food-processing operations.
Pharmaceutical Manufacturing
Pharmaceutical processes can use vacuum systems for drying, filtration, solvent recovery, concentration, and other controlled processing applications.
Chemical Processing
Vacuum pumps can support distillation, evaporation, drying, degassing, and vapor handling in chemical production.
Electronics Manufacturing
Vacuum technology is important in semiconductor processing, coating, drying, and other electronics-related manufacturing processes.
Material Handling
Vacuum pumps can support pneumatic conveying and vacuum lifting systems for handling powders, granules, sheets, and other materials.
Plastics and Rubber Processing
Vacuum systems can be integrated into extrusion, degassing, drying, molding, and other polymer-processing applications.
Vacuum Level and Pumping Speed
Two important parameters when evaluating vacuum equipment are ultimate vacuum and pumping speed.
Ultimate vacuum describes the lowest pressure that a pump can theoretically achieve under specified conditions. Pumping speed indicates how quickly the system can remove gas at a particular pressure.
| Parameter | Meaning |
|---|---|
| Ultimate vacuum | Lowest achievable pressure under specified conditions |
| Pumping speed | Gas removal capacity over time |
| Inlet pressure | Pressure at the pump inlet |
| Exhaust pressure | Pressure at the pump outlet |
| Gas load | Quantity of gas entering the system |
Actual performance depends on piping, leakage, temperature, gas composition, and other system conditions.
Advantages of Industrial Vacuum Pumps
Industrial vacuum pumps can provide several process benefits:
- Controlled low-pressure environments
- Continuous gas removal
- Support for vacuum drying
- Improved process control
- Compatibility with automated systems
- Different technologies for different pressure ranges
- Support for enclosed manufacturing processes
- Integration with centralized vacuum systems
The appropriate benefits depend on the pump type and application.
How to Select Industrial Vacuum Pumps
Selecting a vacuum pump requires more than comparing pressure specifications. The complete process should be evaluated.
Important factors include:
- Required vacuum level
- Pumping speed
- Gas composition
- Vapor content
- Operating temperature
- Contamination levels
- Continuous or intermittent operation
- Chemical compatibility
- Noise requirements
- Cooling requirements
- Maintenance requirements
- Available installation space
For processes containing corrosive chemicals, condensable vapors, dust, or other contaminants, pump construction and filtration requirements should receive particular attention.
Maintenance Considerations
Regular maintenance helps maintain vacuum performance and equipment reliability.
Typical maintenance activities include:
- Checking pump oil where applicable
- Inspecting seals and gaskets
- Cleaning filters
- Checking inlet piping
- Inspecting bearings
- Monitoring operating temperature
- Checking vibration
- Inspecting valves
- Measuring vacuum performance
- Reviewing unusual noise or pressure changes
Maintenance schedules should follow the equipment manufacturer's technical documentation and the operating conditions of the process.
Industrial Vacuum Pump Systems
A complete vacuum installation may contain multiple pumps, receivers, filters, valves, gauges, controllers, and piping. Centralized vacuum systems can distribute vacuum capacity across several production processes.
Automated controls can monitor pressure and pump operation while providing alarms for abnormal conditions. Variable-speed drives can also be incorporated into certain systems to adjust pump operation according to process demand.
Conclusion
Industrial vacuum pumps are essential components in many manufacturing and processing systems that require controlled low-pressure environments. Rotary vane, liquid ring, dry, screw, and piston technologies provide different operating characteristics for specific process requirements.
The appropriate pump depends on vacuum level, pumping speed, gas composition, vapor load, contamination, operating conditions, and maintenance requirements. Evaluating the complete vacuum system rather than the pump alone can help achieve reliable and consistent process performance.
Related Post...
Industrial Dosing Pumps: Types, Working, Applications & Selection
Updated: September 19, 2026
Read More
Boiler Circulation Pumps: Types, Working, Applications & Selection
Updated: September 19, 2026
Read More
Industrial Gear Pumps: Types, Working, Applications & Selection
Updated: September 19, 2026
Read More