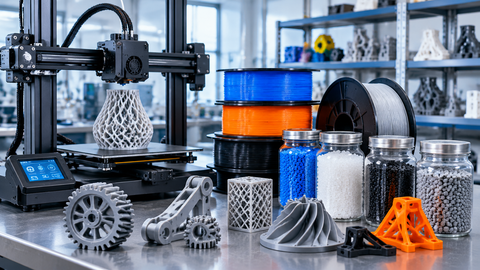
Industrial 3D Printing Materials: Selection Guide and Properties
Industrial 3D printing materials are metals, polymers, ceramics, and composite feedstocks used to manufacture functional components through additive manufacturing.
Each material offers a distinct combination of mechanical strength, thermal resistance, chemical compatibility, weight, surface quality, and processing requirements. Selecting the right material requires matching these properties to the part's operating environment, manufacturing process, and performance requirements.
Material selection also affects dimensional accuracy, production consistency, post-processing, inspection, and long-term component reliability. Understanding these trade-offs helps engineers choose suitable materials for industrial prototypes, tooling, production components, and specialized applications.
Quick Facts About Industrial 3D Printing Materials
Feature | Description |
|---|---|
Main material categories | Metals, thermoplastics, photopolymers, ceramics, and composites |
Common metal materials | Stainless steel, titanium alloys, aluminum alloys, nickel-based alloys |
Common polymer materials | PLA, ABS, PETG, nylon, polycarbonate, PEEK, and PEKK |
Common resin materials | Standard, tough, flexible, and engineering photopolymers |
Common ceramic materials | Alumina, zirconia, and silicon carbide in suitable processes |
Material feedstock forms | Filament, pellets, liquid resin, metal powder, ceramic powder, and wire |
Main selection criteria | Strength, temperature resistance, chemical compatibility, accuracy, and durability |
Common industrial applications | Aerospace, automotive, medical devices, tooling, energy, and manufacturing |
Important consideration | Properties depend on material grade, printing process, orientation, and post-processing |
What Are Industrial 3D Printing Materials?
Industrial 3D printing materials are feedstocks formulated for additive manufacturing processes that create components layer by layer. Depending on the technology, the feedstock may be a polymer filament, thermoplastic granules, liquid photopolymer resin, metal powder, ceramic powder, or wire.
These materials are engineered to behave predictably during deposition, melting, curing, bonding, or sintering. Their properties influence whether the resulting component can withstand mechanical loads, repeated heating, chemical exposure, friction, vibration, or dimensional tolerances.
Unlike conventional material selection, additive manufacturing requires engineers to evaluate both the material itself and the interaction between the material and the printing process. Two parts made from the same nominal polymer or alloy can exhibit different properties because of build orientation, porosity, layer bonding, thermal history, and post-processing.
Why Industrial 3D Printing Material Selection Matters
Material selection determines whether a printed component performs reliably in its intended environment. A material that works well for a visual prototype may be unsuitable for a load-bearing bracket, a high-temperature fixture, or a chemically exposed industrial component.
Choosing an appropriate material can help manufacturers:
Meet mechanical and thermal performance requirements.
Reduce unnecessary component weight.
Produce complex internal channels and customized geometries.
Manufacture replacement components and specialized tooling.
Reduce machining waste for suitable component designs.
Support short production runs and design iterations.
Improve corrosion resistance or wear performance where the selected material permits it.
Establish repeatable manufacturing and inspection procedures.
The highest-strength material is not automatically the best choice. A lighter polymer may meet the requirements of a fixture, while a metal alloy may be necessary for a component exposed to high temperatures or substantial mechanical loads.
Understanding Industrial 3D Printing Materials
Simple Explanation
Consider an industrial mounting bracket. If the bracket holds a lightweight sensor inside a protected enclosure, a suitable engineering polymer may provide adequate stiffness and durability. If it supports a heavy assembly exposed to elevated temperatures, a metal alloy may be more appropriate.
The material must also match the printing technology. A metal powder designed for laser-based powder bed fusion cannot simply be substituted for polymer filament in a material extrusion printer. Each process requires compatible feedstock characteristics and operating conditions.
Material Properties Versus Printed-Part Properties
Material datasheets provide useful starting information, but they do not necessarily represent the performance of a finished printed component.
Important distinctions include:
Feedstock properties: Characteristics of the unprocessed filament, powder, resin, or other material.
Intrinsic material properties: Characteristics associated with the material's composition and condition.
Printed-part properties: Performance of the component after the selected manufacturing process.
Post-processed properties: Characteristics after heat treatment, curing, machining, infiltration, or other finishing operations.
For engineering applications, test results should reflect the relevant manufacturing process and the intended direction of loading whenever possible.
How Industrial 3D Printing Material Selection Works
Step 1: Define the Component's Function
Start by identifying what the component must do. Determine whether it is a prototype, fixture, housing, structural component, fluid-handling part, thermal component, or wear-resistant tool.
Clarify whether the part will carry a static load, experience repeated movement, contact food or biological materials, or operate in a controlled environment.
Step 2: Identify Operating Conditions
Document the temperatures, loads, vibration, moisture, chemical exposure, ultraviolet exposure, and expected operating life. For moving components, friction and wear may be as important as tensile strength.
For safety-critical components, establish applicable design requirements and qualification procedures before selecting a feedstock.
Step 3: Shortlist Compatible Material Families
Use the operating conditions to narrow the options to metals, polymers, ceramics, or composites. Then identify grades compatible with the required additive manufacturing process.
For example, a heat-resistant polymer may suit a lightweight component operating in a demanding environment, while a nickel-based alloy may be more appropriate for certain high-temperature metal applications.
Step 4: Evaluate Mechanical and Physical Properties
Compare tensile strength, stiffness, elongation, impact behavior, density, thermal expansion, thermal conductivity, and chemical resistance as relevant to the application.
Avoid comparing datasheet values without checking the test method, specimen orientation, processing condition, and environmental conditions.
Step 5: Confirm Printing and Post-Processing Requirements
Determine whether the material requires a heated build chamber, support structures, stress relief, curing, sintering, hot isostatic pressing, machining, or surface finishing.
These requirements influence dimensional accuracy, manufacturing complexity, production consistency, and final performance.
Step 6: Validate the Finished Component
Use representative test specimens or component-level testing to verify the properties that matter. Inspection may include dimensional measurement, mechanical testing, surface evaluation, and nondestructive examination where appropriate.
For critical applications, validation should cover the material, process parameters, post-processing, and quality controls as a complete manufacturing route.
Industrial 3D Printing Material Selection Workflow Table
Stage | Main Activity | Output |
|---|---|---|
Application definition | Identify function and service conditions | Engineering requirements |
Environmental assessment | Evaluate heat, chemicals, moisture, and wear | Operating limits |
Material screening | Compare candidate material families | Shortlist |
Property comparison | Review relevant mechanical and physical data | Performance assessment |
Process compatibility | Match feedstock to printing technology | Feasible manufacturing route |
Post-processing review | Define finishing and treatment requirements | Process plan |
Validation | Inspect and test representative parts | Evidence of suitability |
Main Categories of Industrial 3D Printing Materials
Metal Alloys
Metal alloys are used when components require a combination of strength, stiffness, thermal performance, or environmental resistance that a polymer or ceramic may not provide. Common options include stainless steel, aluminum alloys, titanium alloys, cobalt-chromium alloys, and nickel-based superalloys.
Metal additive manufacturing processes include powder bed fusion and directed energy deposition. Binder jetting can also produce metal parts, generally followed by debinding and sintering. The required process determines the feedstock form and the subsequent treatment needed to achieve the intended properties.
Thermoplastics
Thermoplastics soften when heated and solidify as they cool, allowing them to be processed using technologies such as material extrusion and polymer powder bed fusion. Common materials include ABS, nylon, polycarbonate, polypropylene, and high-performance polymers such as PEEK and PEKK.
They are useful for housings, jigs, fixtures, ducts, lightweight components, and selected functional parts. Their properties vary substantially by grade, reinforcement, printing method, and build orientation.
Photopolymer Resins
Photopolymer resins are liquid formulations that harden when exposed to an appropriate light source. They are commonly used in vat photopolymerization processes, including stereolithography and digital light processing.
Resins can produce detailed features and smooth surfaces, making them useful for patterns, housings, models, and selected engineering components. Their limitations may include aging, brittleness, heat sensitivity, and changes in properties caused by curing and environmental exposure.
Ceramic Materials
Ceramic feedstocks are used to manufacture parts requiring properties such as high-temperature stability, hardness, wear resistance, electrical insulation, or chemical resistance. Common industrial ceramics include alumina and zirconia, while silicon carbide is used in suitable specialized processes.
Many ceramic additive manufacturing routes require debinding and sintering. These steps can cause shrinkage and require careful process control to achieve the intended dimensions and microstructure.
Composite Materials
Composite feedstocks combine a matrix material with reinforcement such as carbon fibers, glass fibers, or ceramic particles. In polymer additive manufacturing, fiber reinforcement can improve stiffness or strength in particular directions, depending on the material and process.
Composite properties are highly dependent on reinforcement type, fiber length, fiber orientation, matrix adhesion, and the printed geometry. Reinforcement does not guarantee that a printed part will outperform every unreinforced alternative.
Industrial 3D Printing Materials Comparison Table
Material Category | Main Strengths | Typical Limitations | Common Applications |
|---|---|---|---|
Metal alloys | Strength, stiffness, and application-specific heat resistance | Powder handling, support removal, and post-processing requirements | Aerospace components, tooling, industrial parts |
Standard thermoplastics | Lightweight construction and broad design flexibility | Heat resistance and strength vary by grade | Prototypes, housings, fixtures |
High-performance thermoplastics | Potentially high thermal and mechanical performance | Specialized processing conditions | Engineering components and demanding environments |
Photopolymer resins | Fine detail and smooth surfaces | Aging and mechanical performance vary by formulation | Detailed prototypes, patterns, selected functional parts |
Technical ceramics | Hardness, thermal stability, and selected chemical properties | Brittleness and demanding post-processing | Insulators, wear parts, thermal components |
Fiber-reinforced composites | Improved stiffness or strength in selected directions | Anisotropy and more complex material behavior | Fixtures, lightweight structures, tooling |
Industrial Metal 3D Printing Materials and Their Properties
Metal selection requires attention to alloy composition, heat treatment, corrosion conditions, fatigue behavior, and the manufacturing process. A material's conventional wrought or cast properties should not automatically be assumed for an additively manufactured part.
Stainless Steel
Stainless steel alloys are widely used when corrosion resistance, mechanical strength, and durability are required. Common additive manufacturing grades include 316L and 17-4 PH, although their properties and processing requirements differ.
Strengths: Corrosion resistance for suitable environments, useful mechanical performance, and broad industrial applicability.
Limitations: Corrosion behavior depends on the alloy, exposure conditions, surface finish, and post-processing.
Applications: Fluid-handling components, industrial tooling, brackets, housings, and selected chemical-processing equipment.
Aluminum Alloys
Aluminum alloys are attractive for applications requiring low mass and useful strength. Their relatively low density makes them relevant to weight-sensitive industrial structures, heat-management components, and transportation applications.
Strengths: Low density, machinability in suitable conditions, and potential for lightweight designs.
Limitations: Alloy-specific cracking, residual stress, thermal behavior, and post-processing can affect performance.
Applications: Aerospace structures, lightweight fixtures, housings, and thermal-management components.
Titanium Alloys
Titanium alloys combine high specific strength with corrosion resistance in many environments. Ti-6Al-4V is a commonly used alloy in metal additive manufacturing.
Strengths: High strength relative to weight and useful corrosion resistance.
Limitations: Feedstock handling, processing control, and post-processing require careful management.
Applications: Aerospace components, specialized industrial parts, and qualified medical applications.
Nickel-Based Superalloys
Nickel-based alloys are used in demanding thermal and mechanical environments. Some grades retain useful strength at elevated temperatures and resist oxidation or corrosion under specified conditions.
Strengths: High-temperature performance and application-specific environmental resistance.
Limitations: Processing can be demanding, and material removal or finishing may be difficult.
Applications: Turbomachinery components, energy systems, and selected high-temperature industrial equipment.
Cobalt-Chromium Alloys
Cobalt-chromium alloys can provide high wear resistance and useful corrosion performance in suitable environments. Their use depends on the exact composition, manufacturing process, and qualification requirements.
Strengths: Hardness, wear resistance, and useful performance in selected demanding applications.
Limitations: Machining and finishing may be challenging, and application-specific biocompatibility or regulatory requirements must be verified.
Applications: Selected medical components, dental parts, and specialized industrial components.
Industrial Polymer 3D Printing Materials and Their Properties
Polymer selection involves more than comparing tensile strength. Engineers must evaluate stiffness, impact resistance, creep, moisture absorption, thermal distortion, chemical compatibility, and the effects of repeated loading.
PLA
Polylactic acid is a thermoplastic frequently used for concept models and basic prototypes. It is generally straightforward to process using material extrusion.
Strengths: Good detail for many prototype applications and convenient processing.
Limitations: Limited suitability for sustained high temperatures and demanding long-term mechanical loads.
Applications: Visual models, fit checks, design studies, and non-demanding fixtures.
ABS
Acrylonitrile butadiene styrene is used for functional prototypes, housings, and selected engineering parts. Its impact behavior and heat performance depend on the grade and manufacturing conditions.
Strengths: Useful toughness and broad application flexibility.
Limitations: Warping, layer adhesion, and emissions during processing require attention.
Applications: Enclosures, covers, housings, and general engineering prototypes.
PETG
Polyethylene terephthalate glycol-modified is often selected for parts requiring a balance of toughness, processability, and chemical resistance under suitable conditions.
Strengths: Useful impact performance and relatively accessible processing.
Limitations: Heat resistance, creep, and chemical compatibility vary by grade.
Applications: Covers, brackets, containers, and functional prototypes.
Nylon and Polyamide
Nylon materials, including PA12 and PA11, are widely used in industrial polymer additive manufacturing. They can provide useful toughness and fatigue behavior, depending on the grade and process.
Strengths: Good potential for durable, lightweight functional parts.
Limitations: Moisture absorption can affect dimensions and mechanical properties; some grades also require careful powder or filament conditioning.
Applications: Clips, housings, ducts, functional assemblies, and selected end-use components.
Polycarbonate
Polycarbonate is valued for impact resistance and relatively high heat performance compared with many general-purpose thermoplastics.
Strengths: Toughness and useful thermal performance in appropriate grades.
Limitations: Processing can be sensitive to moisture, temperature control, and build conditions.
Applications: Protective covers, fixtures, enclosures, and functional engineering parts.
PEEK and PEKK
PEEK and PEKK are high-performance thermoplastics used in applications requiring demanding combinations of thermal, chemical, and mechanical properties.
Strengths: Potential for elevated-temperature performance and chemical resistance.
Limitations: Specialized processing equipment and strict thermal control are often required.
Applications: Aerospace components, industrial fixtures, chemical-exposed parts, and selected medical applications subject to qualification.
Industrial 3D Printing Resin Properties and Applications
Photopolymer resins should be selected according to their intended formulation rather than treated as one uniform material category. Resin properties depend on the chemistry, exposure conditions, post-curing, and environmental aging.
Standard Resins
Standard resins are often used when appearance, dimensional detail, and surface quality are more important than exceptional mechanical durability. They are suitable for many visual models and fit-check prototypes.
Tough and Impact-Resistant Resins
These formulations are intended to improve resistance to impact or mechanical loading compared with standard resins. Their performance varies by product and should be validated for the intended use.
Flexible and Elastomeric Resins
Flexible resins can produce parts that bend or deform under load. Engineers should evaluate tear resistance, compression behavior, fatigue, and aging before using them in functional seals or repeated-motion components.
High-Temperature Resins
These resins are formulated for applications requiring greater heat resistance than standard formulations. Their usable temperature depends on the specific formulation, curing process, applied load, and duration of exposure.
Ceramic 3D Printing Materials and Their Properties
Ceramic materials are useful when hardness, wear resistance, electrical insulation, or high-temperature performance is required. Their mechanical behavior differs from that of metals and polymers, especially under impact or tensile loading.
Alumina
Alumina is commonly used for electrical insulation, wear-resistant components, and selected chemical-processing applications. It offers high hardness and good thermal stability, but its suitability depends on porosity, purity, geometry, and the finished part's mechanical loading.
Zirconia
Zirconia can provide high hardness and, in suitable formulations, improved fracture toughness compared with many conventional ceramics. Its performance depends on composition, stabilization, microstructure, and processing history.
Silicon Carbide
Silicon carbide is valued for hardness, wear resistance, and high-temperature performance in suitable applications. Additive manufacturing routes and densification requirements depend on the specific process and component geometry.
Ceramic Processing Considerations
Ceramic parts may undergo binder removal, sintering, infiltration, or other densification steps. Shrinkage, porosity, cracks, and dimensional changes must be considered when designing the component and planning inspection.
Composite 3D Printing Materials and Reinforcement Types
Composite materials offer a way to tailor stiffness, weight, and other properties beyond what an unreinforced matrix may provide. Their behavior depends on the reinforcement architecture and how effectively loads transfer between the reinforcement and the matrix.
Chopped-Fiber-Reinforced Polymers
Short carbon or glass fibers may be mixed into a polymer matrix. They can improve stiffness and dimensional stability in suitable formulations, but the extent of improvement depends on fiber content, orientation, and process conditions.
Continuous-Fiber-Reinforced Materials
Some additive manufacturing processes place continuous fibers within a polymer matrix. This can produce high stiffness and strength along selected fiber directions, but performance is highly directional and requires careful structural design.
Ceramic-Filled and Particle-Reinforced Materials
Particles can change stiffness, wear behavior, thermal properties, or surface characteristics. High filler content may also affect flow, bonding, brittleness, and process compatibility.
Industrial 3D Printing Material Selection Requirements
Requirement | Properties to Evaluate | Key Question |
|---|---|---|
Mechanical loading | Tensile strength, stiffness, fatigue, impact behavior | What loads will the component experience? |
Thermal exposure | Heat resistance, thermal expansion, creep | What temperatures and durations are expected? |
Chemical exposure | Corrosion or chemical compatibility | Which substances will contact the part? |
Weight constraints | Density and structural stiffness | Is mass reduction a priority? |
Dimensional accuracy | Shrinkage, warping, orientation effects | What tolerances must be maintained? |
Surface and wear | Surface roughness, hardness, abrasion | Will the part slide, rub, or contact other parts? |
Electrical function | Conductivity or insulation | Must the component conduct or isolate electricity? |
Regulatory requirements | Traceability, biocompatibility, material qualification | What standards or approvals apply? |
Production repeatability | Feedstock consistency and process control | Can the required properties be reproduced? |
Industrial 3D Printing Materials vs. CNC Machining and Injection Molding
Industrial 3D printing is one of several manufacturing approaches available for producing polymer and metal components. The most appropriate process depends on component geometry, material requirements, production volume, tolerances, and inspection needs.
Factor | Industrial 3D Printing | CNC Machining | Injection Molding |
|---|---|---|---|
Manufacturing method | Builds parts layer by layer | Removes material from a workpiece | Injects molten material into a mold |
Geometric complexity | Supports many complex internal and external features | Depends on tool access and machining strategy | Depends on mold design and part geometry |
Material options | Process-specific metals, polymers, ceramics, and composites | Broad range of machinable materials | Primarily mold-compatible polymers and selected other materials |
Material waste | Can reduce waste for suitable geometries | Generates chips and removed material | Produces runners and other process waste depending on design |
Production volume | Particularly useful for prototypes, customization, and selected production runs | Useful for prototypes and production components | Often advantageous for large runs of suitable parts |
Tooling requirements | Often limited dedicated tooling | Requires appropriate workholding and cutting tools | Requires a dedicated mold |
Part properties | Depend on process, orientation, and post-processing | Depend on material condition and machining | Depend on material, mold conditions, and processing |
Main limitation | Process constraints and potentially demanding post-processing | Tool access and material-removal requirements | Mold development and design constraints |
Neither additive manufacturing nor conventional manufacturing is universally superior. Some components are best printed, while others are more suitable for machining or molding. Hybrid production can also combine printed geometries with machined surfaces or conventional assemblies.
Benefits and Advantages of Industrial 3D Printing Materials
The value of additive manufacturing comes from matching the material to a design and production method that take advantage of the process.
Design flexibility: Supports complex geometries, internal channels, lattice structures, and part consolidation where technically feasible.
Material-specific performance: Offers options ranging from lightweight polymers to high-strength metal alloys and technical ceramics.
Reduced tooling dependence: Many parts can be produced without dedicated molds or specialized forming tools.
Rapid design iteration: Engineers can evaluate alternative geometries and material grades during development.
Customization: Supports components with individualized shapes or application-specific features.
Lightweight engineering: Suitable materials and optimized geometries can reduce component mass.
Localized production: Digital part files can support production closer to the point of use when the required equipment and feedstock are available.
Selected waste reductions: Building only the required geometry can reduce material removal compared with some subtractive processes, although supports, unused feedstock, and post-processing waste still matter.
These advantages must be evaluated against the required component performance, production economics, qualification burden, and environmental impact of the complete manufacturing route.
Industry Applications of Industrial 3D Printing Materials
Aerospace and Aviation
Titanium alloys, aluminum alloys, nickel-based alloys, and high-performance polymers are used in selected aerospace applications. Material selection considers strength-to-weight ratio, thermal exposure, fatigue, traceability, and stringent part qualification requirements.
Complex internal channels and consolidated geometries can be beneficial, but critical flight components require validated manufacturing processes and appropriate inspection.
Automotive and Transportation
Industrial polymer and metal printing supports prototype development, manufacturing fixtures, ducts, brackets, lightweight structures, and selected production parts. Nylon, reinforced polymers, aluminum alloys, and stainless steels may be appropriate depending on the application.
Temperature exposure, vibration, fatigue, dimensional consistency, and production volume are important selection factors.
Medical and Dental Manufacturing
Titanium alloys, cobalt-chromium alloys, selected polymers, and specialized photopolymers are used in particular medical and dental applications. Material suitability depends on the intended contact, manufacturing process, sterilization requirements, and applicable regulatory controls.
A material's general reputation for biocompatibility does not establish that every printed component is safe for clinical use.
Industrial Tooling and Manufacturing
Polymers, reinforced composites, tool steels, and other metal alloys can be used to produce jigs, fixtures, assembly aids, conformal cooling inserts, and selected replacement components. The required stiffness, wear resistance, temperature tolerance, and dimensional stability determine the most suitable option.
Energy and Power Generation
Nickel-based alloys, stainless steels, titanium alloys, and selected ceramics are relevant to components exposed to heat, corrosion, pressure, or demanding operating environments. Material and process qualification are especially important where failure could affect system integrity.
Chemical Processing
Corrosion-resistant alloys and compatible polymers can be considered for selected housings, fluid-handling components, fixtures, and specialized parts. Material compatibility must be evaluated against the actual chemical concentration, temperature, pressure, and exposure duration.
Electronics and Electrical Manufacturing
Polymers, selected resins, ceramics, and specialized conductive composites can be used for enclosures, fixtures, insulation components, and prototypes. Electrical resistance, dielectric behavior, heat dissipation, and dimensional stability must match the application.
Industrial 3D Printing Materials Industry Applications Table
Industry | Common Material Families | Example Applications | Main Selection Priority |
|---|---|---|---|
Aerospace | Titanium, aluminum, nickel alloys, high-performance polymers | Lightweight parts and qualified thermal components | Strength, fatigue, traceability |
Automotive | Nylon, reinforced polymers, aluminum, stainless steel | Fixtures, ducts, brackets, prototypes | Durability and repeatability |
Medical and dental | Titanium, cobalt-chromium, qualified polymers and resins | Specialized implants, dental parts, anatomical models | Biocompatibility and regulatory qualification |
Industrial manufacturing | Reinforced polymers, tool steels, stainless steel | Jigs, fixtures, tooling inserts | Wear resistance and dimensional stability |
Energy | Nickel alloys, stainless steel, ceramics | Selected thermal and corrosion-resistant components | Temperature and environmental resistance |
Chemical processing | Compatible alloys and polymers | Selected fluid-handling parts and fixtures | Chemical compatibility |
Electronics | Polymers, ceramics, specialized composites | Enclosures, insulators, assembly fixtures | Electrical and thermal properties |
Industry Standards and Safety for Industrial 3D Printing Materials
Standards help define material characterization, process qualification, part testing, and safe handling. The applicable requirements depend on the material, additive manufacturing technology, end-use sector, and jurisdiction.
ISO/ASTM 52900
This standard establishes terminology and general principles for additive manufacturing. Consistent terminology helps manufacturers communicate about processes, materials, and production methods.
ISO/ASTM 52907
ISO/ASTM 52907 addresses characterization of metal powders used as additive manufacturing feedstocks. Relevant characteristics include particle-size distribution, chemical composition, morphology, flowability, contamination, documentation, and storage.
ISO/ASTM 52920
ISO/ASTM 52920 addresses qualification principles and requirements for industrial additive manufacturing processes and production sites. It is relevant when establishing controlled industrial production practices.
ISO/ASTM 52908
ISO/ASTM 52908 addresses post-processing, inspection, testing, and qualification considerations for metal parts produced by powder bed fusion. It is particularly relevant when finished-part properties must be verified.
ISO/ASTM 52931
ISO/ASTM 52931 provides general environmental, health, and safety principles for the use of metallic materials in additive manufacturing. Metal powder handling requires particular attention to exposure, contamination, fire, and explosion hazards.
Application-Specific Requirements
Aerospace, medical, automotive, pressure-containing, and other regulated applications may require additional material specifications, quality management controls, process qualification, and traceability.
Standards should be checked for their current editions and applicability before they are used as acceptance criteria. Compliance with a material or process standard alone does not automatically qualify a finished component for a specific use.
Common Industrial 3D Printing Material Challenges and Solutions
Challenge | Possible Cause | Appropriate Response |
|---|---|---|
Warping or distortion | Residual stress, uneven cooling, or unsuitable build conditions | Review process parameters, geometry, and build orientation |
Weak layer bonding | Inadequate fusion, deposition, or curing | Verify process settings and material compatibility |
Porosity in metal parts | Incomplete fusion, trapped gas, or process instability | Review process control and suitable inspection methods |
Inconsistent dimensions | Shrinkage, thermal distortion, or variable processing | Validate compensation, build conditions, and finishing |
Moisture-related defects | Hygroscopic feedstock or unsuitable storage | Follow material-specific drying and storage procedures |
Brittle printed components | Material limitations, defects, or unsuitable orientation | Review grade selection, processing, and load direction |
Surface roughness | Layer structure, particle adhesion, or process limitations | Assess finishing requirements and surface-critical features |
Chemical degradation | Incompatible material or environmental exposure | Validate compatibility under actual operating conditions |
Powder contamination | Poor handling, mixing, or inadequate feedstock control | Maintain segregation, traceability, and handling procedures |
Variable part performance | Inconsistent feedstock, build conditions, or post-processing | Establish process qualification and repeatable inspection |
How to Choose Industrial 3D Printing Materials
The selection process should begin with functional requirements and eliminate unsuitable candidates before comparing secondary advantages. Material datasheets, representative test results, and process-specific qualification evidence should be used together.
Decision Factor | What to Check | Selection Guidance |
|---|---|---|
Component function | Prototype, fixture, structural part, or production component | Match material performance to the actual function |
Load requirements | Static loads, impact, vibration, fatigue | Review strength, stiffness, toughness, and fatigue data |
Temperature | Continuous and intermittent exposure | Confirm operating limits under load |
Chemical environment | Fluids, solvents, acids, alkalis, cleaning agents | Verify compatibility with the exact grade |
Density | Component mass and structural needs | Compare weight with required stiffness and strength |
Geometry | Thin walls, internal channels, fine features | Check process resolution and support requirements |
Surface finish | Mating surfaces, sealing areas, appearance | Include finishing and inspection in the plan |
Manufacturing process | Material extrusion, powder bed fusion, vat photopolymerization, or another process | Confirm feedstock compatibility |
Production volume | Prototype, short run, or recurring production | Compare setup, throughput, and post-processing needs |
Compliance | Industry specifications and traceability | Define acceptance criteria before production |
Lifecycle | Wear, repairability, recycling, and replacement | Evaluate expected operating life and end-of-life handling |
Match the Material to the Application
A practical shortlist can be developed by starting with the dominant requirement:
For lightweight structural parts, evaluate suitable aluminum alloys, titanium alloys, or reinforced polymers.
For demanding thermal environments, investigate qualified metal alloys, technical ceramics, or high-performance polymers.
For fine visual details, consider compatible photopolymer resins.
For durable polymer functional parts, evaluate appropriate nylon or other engineering thermoplastics.
For electrical insulation, assess compatible polymers or ceramics.
For abrasive environments, compare wear-resistant alloys, ceramics, and suitable reinforced materials.
These are starting points rather than universal recommendations. Final selection must account for the process, finished-part properties, and actual service conditions.
Maintenance and Storage Best Practices for 3D Printing Materials
Material handling and storage affect feedstock consistency, printing performance, and finished-part quality. Maintenance practices should follow the requirements of the selected material and manufacturing technology rather than applying one procedure to every feedstock.
Store Materials Under Appropriate Conditions
Moisture-sensitive polymers may require sealed containers, controlled humidity, or drying before processing. Metal powders and ceramic feedstocks should be protected from contamination and stored according to their material-specific handling requirements.
Track Material Grades and Batches
Record material grade, batch identification, storage history, and relevant processing information. Traceability is particularly important when parts must meet specified mechanical, chemical, or regulatory requirements.
Monitor Feedstock Condition
Check for contamination, damaged packaging, moisture exposure, abnormal powder behavior, or expired material where shelf life applies. Reuse and blending of previously processed feedstock should follow validated procedures.
Maintain Printing Equipment
Keep build surfaces, material delivery systems, powder handling equipment, resin containers, and other process-specific components in suitable condition. Equipment maintenance should be coordinated with the approved material and process parameters.
Control Post-Processing
Heat treatment, curing, sintering, machining, and surface finishing can substantially change the final component. Use defined procedures and suitable inspection methods to confirm that the finished part meets its requirements.
Follow Safe Handling Procedures
Fine powders, uncured resins, heated materials, and processing emissions can present health or fire hazards. Use appropriate ventilation, personal protective equipment, containment, and material-specific procedures. Specialized metal powder systems require qualified controls for combustible dust, ignition, and exposure risks.
Limitations of Industrial 3D Printing Materials
Every material family has trade-offs, and additive manufacturing introduces process-related limitations that must be considered alongside material properties.
Directional properties: Some printed parts have different mechanical properties along different build directions.
Surface quality: Layer lines, attached particles, and support marks may require additional finishing.
Dimensional variation: Shrinkage, residual stress, and thermal effects can affect final dimensions.
Material restrictions: Not every alloy, polymer, ceramic, or composite is compatible with every printing process.
Post-processing requirements: Some metal and ceramic components require substantial treatment before reaching their intended properties.
Qualification demands: Critical applications may require extensive testing, traceability, and process control.
Long-term durability: Creep, fatigue, ultraviolet exposure, moisture, and chemical aging can limit service life.
Production constraints: Build capacity, manufacturing speed, feedstock handling, and finishing requirements can limit throughput.
Environmental trade-offs: Energy consumption, unused feedstock, support structures, and material recovery affect the overall environmental impact.
Material selection should therefore be based on demonstrated performance under relevant conditions rather than a single headline property such as tensile strength or heat resistance.
Future Trends in Industrial 3D Printing Materials
Higher-Performance Polymer Formulations
Materials research continues to focus on improved thermal stability, mechanical performance, chemical resistance, and compatibility with industrial printing processes. These developments may expand applications where lightweight polymer parts can meet demanding engineering requirements.
Improved Metal Powder Characterization
More consistent measurement of particle size, morphology, flowability, composition, and feedstock condition supports improved process repeatability. Powder characterization and lifecycle management are particularly relevant to industrial metal additive manufacturing.
Advanced Composites and Functional Materials
Research into fiber reinforcement, ceramic-filled materials, and functionally graded structures aims to tailor properties to local component requirements. Practical performance depends on process capability, material architecture, and validation.
Greater Process Monitoring
Sensors and data analysis are increasingly used to observe manufacturing conditions and identify potential defects. Monitoring can support quality assurance, but it does not replace appropriate material testing or finished-part inspection.
Improved Qualification and Traceability
Industrial adoption increasingly depends on documented process conditions, controlled feedstock, repeatable testing, and traceable production records. These practices are essential when printed components must satisfy strict engineering or regulatory requirements.
Frequently Asked Questions About Industrial 3D Printing Materials
1. What materials are used in industrial 3D printing?
Industrial 3D printing uses metals, thermoplastics, photopolymer resins, ceramics, and composite feedstocks. The available materials depend on the manufacturing technology and the required component properties.
2. Which industrial 3D printing material is strongest?
There is no universally strongest material because strength depends on the loading mode, alloy or polymer grade, manufacturing process, and build orientation. Engineers should compare relevant tensile, compressive, fatigue, and impact data for finished parts rather than relying on one strength value.
3. Which 3D printing materials withstand high temperatures?
Certain nickel-based alloys, stainless steel grades, technical ceramics, and high-performance polymers can suit elevated-temperature applications. Their suitability depends on the actual temperature, duration, applied load, atmosphere, and manufacturing condition.
4. What is the difference between metal and polymer 3D printing materials?
Metal materials generally provide higher stiffness and strength for many structural applications, while polymers often offer lower density and useful flexibility. The appropriate choice depends on load requirements, temperature, chemical exposure, weight, and the capabilities of the selected printing process.
5. Are industrial 3D printing materials suitable for end-use components?
Yes. Qualified metal alloys, engineering polymers, ceramics, and composites can be used for selected functional and production components. Suitability must be established through appropriate design, process control, testing, and inspection.
6. How do engineers compare industrial 3D printing material properties?
Engineers evaluate properties such as tensile strength, stiffness, elongation, impact resistance, density, thermal behavior, chemical compatibility, and fatigue performance. They also verify test methods, build orientation, post-processing, and the conditions under which the data was obtained.
7. Can 3D printing materials be recycled or reused?
Some thermoplastic materials can be reprocessed, and certain metal powders can be recovered for controlled reuse. However, recycling and reuse depend on material degradation, contamination, process requirements, and quality specifications.
8. Why does build orientation affect material properties?
Layer-based manufacturing can produce directional differences in bonding, porosity, fiber alignment, and microstructure. Consequently, a part may perform differently depending on the direction of the applied load relative to its build orientation.
9. Which standards apply to industrial 3D printing materials?
Relevant standards include ISO/ASTM 52900 for terminology and general principles, ISO/ASTM 52907 for metal powder characterization, and ISO/ASTM 52908 for specified aspects of metal powder bed fusion post-processing and inspection. Additional standards may apply according to the material, manufacturing process, and end-use industry.
10. How should industrial 3D printing materials be stored?
Storage requirements vary by material. Moisture-sensitive polymers may need sealed, dry storage, while metal powders require controls for contamination, moisture, ignition, and exposure. Manufacturers should follow the material-specific storage and handling procedures.
Conclusion
Industrial 3D printing material selection requires a balanced assessment of mechanical performance, thermal behavior, chemical compatibility, manufacturing requirements, and finished-part quality. Metals, polymers, ceramics, resins, and composites each offer distinct advantages and limitations. By matching the material to the application and validating the complete manufacturing process, engineers can produce components that meet defined performance, reliability, and quality requirements.
Related Post...