Industrial Chemical Overview for Process and Material Needs
Industrial chemicals play an essential role in manufacturing, material processing, surface treatment, cleaning, and product development.
Their properties influence how materials behave, how efficiently production processes operate, and whether finished products meet required performance standards.
Different industries rely on chemicals for different purposes. A metal processing facility may require corrosion inhibitors and surface treatment compounds, while a plastics manufacturer may use solvents, additives, catalysts, or processing aids. Selecting suitable chemicals requires understanding both the intended application and the conditions under which they will be used.
Understanding industrial chemical categories, performance characteristics, compatibility requirements, and supplier evaluation criteria helps businesses make informed technical decisions. The right selection process can support product quality, operational consistency, equipment protection, and workplace safety.
How Industrial Chemicals Support Manufacturing Processes
Industrial chemicals are substances used in industrial operations to produce, transform, clean, protect, or improve materials and products. They may serve as primary ingredients, processing agents, surface treatments, catalysts, or maintenance chemicals.
Their functions vary considerably. Acids and alkalis can adjust pH or remove unwanted deposits, solvents can dissolve specific substances, and surfactants can improve cleaning by helping liquids interact with oils and other contaminants. Polymers and additives can modify material properties, while corrosion inhibitors help reduce degradation under suitable operating conditions.
Chemical performance depends on concentration, temperature, pressure, exposure time, and interactions with other substances. A formulation that performs effectively in one process may be unsuitable for another because of differences in material composition or operating conditions.
For industrial buyers, the objective is not simply to identify a chemical with the desired function. It is to find a formulation that meets technical requirements while remaining compatible with the production environment.
Major Categories of Industrial Chemicals
Industrial chemicals can be classified according to their composition, function, or application. Understanding these categories helps procurement and engineering teams narrow their options before evaluating individual formulations.
Process and Treatment Chemicals
Process chemicals support activities such as cleaning, separation, pH adjustment, water treatment, and surface preparation. Depending on the application, they may help remove contaminants, control mineral deposits, improve process stability, or prepare materials for subsequent manufacturing stages.
Water treatment chemicals, for example, can help manage scaling, corrosion, suspended particles, or microbial growth in appropriate industrial systems. Their suitability depends on water chemistry, equipment design, treatment objectives, and discharge requirements.
Solvents, Additives, and Formulation Ingredients
Solvents are used in applications such as coatings, cleaning, extraction, and chemical manufacturing. Selection depends on factors including solvency, evaporation behavior, compatibility, worker exposure, and environmental requirements.
Additives modify the properties or processing behavior of another material. In plastics, coatings, adhesives, and specialty formulations, these substances may influence flexibility, stability, viscosity, durability, or resistance to degradation.
The intended function must be assessed alongside interactions with the base material. An additive that improves one characteristic may affect another, making formulation testing important before large-scale implementation.
Corrosion Inhibitors and Surface Treatment Chemicals
Industrial equipment and components may be exposed to moisture, salts, acids, or other corrosive environments. Corrosion inhibitors and protective treatment chemicals help control material degradation under defined conditions.
Surface treatment chemicals are also used to prepare metals and other substrates before coating, bonding, or finishing. Their effectiveness depends on the substrate, surface condition, treatment process, and required final properties.
Choosing Chemicals for Specific Material Requirements
Chemical selection begins with the material being processed and the performance expected from the final product. Metals, polymers, ceramics, glass, and composite materials respond differently to chemical exposure, so compatibility must be evaluated rather than assumed.
For example, a cleaning agent suitable for stainless steel may damage certain aluminum surfaces or polymer components. Similarly, a solvent that dissolves a coating effectively may also affect seals, adhesives, or nearby plastic parts.
Industrial teams should establish several requirements before comparing formulations:
- Material compatibility: Confirm how the chemical interacts with substrates, seals, coatings, and other exposed components.
- Process conditions: Identify operating temperature, concentration, contact time, pressure, and any relevant process variations.
- Performance requirements: Define the desired outcome, such as contaminant removal, surface protection, material stability, or improved processing.
- Safety and handling: Review exposure risks, storage conditions, protective equipment, and emergency procedures.
- Environmental requirements: Assess waste handling, wastewater compatibility, emissions, and applicable regulatory obligations.
Laboratory testing and controlled production trials can help identify unexpected interactions before full implementation. Testing should reflect realistic operating conditions wherever practical.
How to Evaluate Industrial Chemical Suppliers
Selecting a supplier involves more than comparing product descriptions. Industrial buyers need confidence that the supplied formulation meets specifications, remains consistent between batches, and can be handled safely within the intended operation.
A useful evaluation starts with technical documentation. Product specifications, safety data sheets, certificates of analysis where applicable, storage instructions, and compatibility guidance help establish whether a chemical meets operational requirements.
Supplier capability also matters. Depending on the application, relevant considerations may include batch traceability, quality management systems, technical support, packaging options, delivery reliability, and the ability to provide consistent product documentation.
When comparing industrial chemical suppliers, assess the following factors:
| Evaluation factor | What to verify |
|---|---|
| Product specifications | Chemical identity, concentration, purity, and relevant performance parameters |
| Quality assurance | Batch consistency, testing procedures, and traceability |
| Technical support | Application guidance, compatibility information, and troubleshooting assistance |
| Safety documentation | Current safety data sheets, handling instructions, and storage requirements |
| Supply continuity | Production capacity, lead times, packaging, and contingency arrangements |
| Regulatory suitability | Applicable chemical restrictions, labeling requirements, and industry obligations |
Not every supplier will provide the same level of technical support or documentation. Requirements should reflect the chemical's risk profile and the consequences of inconsistent product quality.
For critical manufacturing processes, a qualified alternative supplier may also help reduce supply disruption. However, replacement chemicals should not be substituted solely because they appear similar. Differences in composition can affect process performance, equipment compatibility, and finished-product quality.
Safety, Storage, and Regulatory Considerations
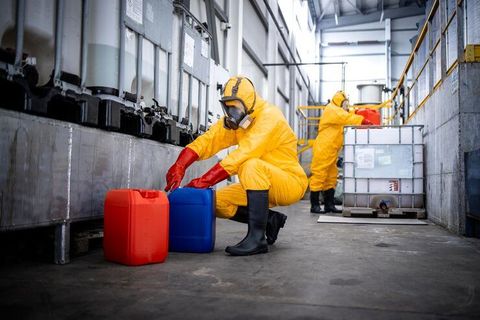
Industrial chemicals can present hazards such as corrosivity, flammability, toxicity, or harmful environmental effects. The actual risks depend on the substance, concentration, exposure route, handling conditions, and quantity involved.
A current safety data sheet provides important information about hazards, protective measures, storage, spill response, and emergency procedures. Employees should receive training appropriate to their responsibilities, and chemicals should be stored according to their specific compatibility and handling requirements.
Incompatible substances may react dangerously if mixed or stored together. Facilities should therefore establish appropriate segregation procedures, labeling practices, ventilation controls, and spill-management arrangements.
Regulatory obligations vary by jurisdiction and chemical application. Businesses may need to consider workplace safety rules, hazardous-material transport requirements, environmental permits, chemical inventories, and restrictions on particular substances. These requirements should be confirmed for the relevant location and process rather than assumed to be universal.
Frequently Asked Questions
What factors determine whether an industrial chemical is suitable?
Suitability depends on the intended function, material compatibility, operating conditions, performance requirements, safety profile, and applicable regulations. Technical documentation and controlled testing help confirm whether a formulation meets the requirements.
Why is chemical compatibility important in manufacturing?
Incompatible chemicals can damage equipment, degrade materials, interfere with coatings, or create unwanted reactions. Compatibility assessment helps protect product quality and maintain reliable process performance.
What documentation should industrial chemical buyers request?
Depending on the product and application, useful documents include technical specifications, safety data sheets, certificates of analysis, storage instructions, and relevant regulatory or quality documentation.
Can one industrial chemical replace another with a similar function?
Not necessarily. Chemicals with similar intended uses may differ in concentration, composition, reactivity, compatibility, and operating requirements. Any substitution should undergo appropriate technical and safety evaluation.
What should businesses consider when comparing chemical suppliers?
Evaluate product consistency, documentation, technical expertise, quality controls, delivery reliability, regulatory suitability, and the supplier's ability to meet ongoing operational requirements.
Conclusion
Industrial chemical selection requires a clear understanding of process objectives, material compatibility, operating conditions, and safety requirements. Different formulations may perform similar functions but produce different results under specific industrial conditions.
By defining technical requirements, evaluating supplier capabilities, reviewing documentation, and conducting appropriate compatibility tests, businesses can make more informed decisions. A disciplined selection process supports consistent production, responsible chemical handling, and reliable material performance.
Related Post...
Corporate Gifting Solutions Discover Ideas That Strengthen Client and Employee Connections
Updated: October 26, 2026
Read More