Roller Conveyor System Solutions for Smooth Material Handling
Moving materials efficiently is essential for warehouses, manufacturing facilities, distribution centers, and packaging operations.
A roller conveyor system helps businesses transport products between workstations while reducing manual handling and supporting consistent material flow.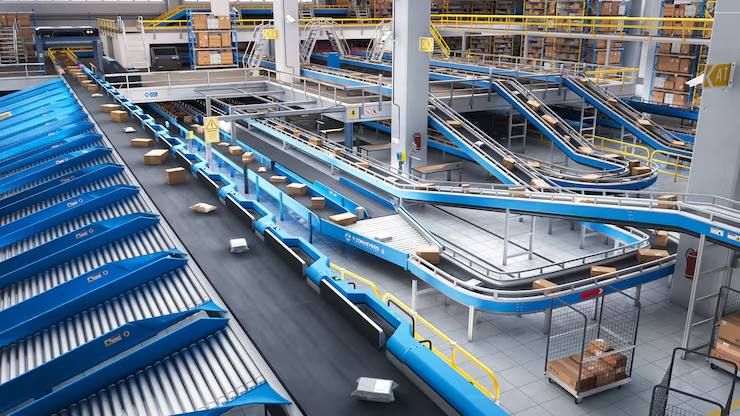
As industrial operations handle increasing product volumes and more complex workflows, conveyor equipment plays an important role in improving operational coordination. Roller conveyors are particularly useful for moving cartons, containers, pallets, and other items across defined routes.
Understanding roller conveyor solutions helps businesses evaluate suitable configurations, operating requirements, and equipment capabilities. Choosing the right system involves considering load characteristics, facility layout, movement requirements, and integration with other material handling equipment.
How Roller Conveyor Systems Support Material Movement
A roller conveyor system uses a series of cylindrical rollers mounted within a supporting frame to move materials along a designated path. Products travel across the rollers through gravity, manual force, or powered mechanical movement.
These systems are commonly installed in receiving areas, production lines, sorting facilities, and dispatch operations. They help connect different stages of material handling without requiring employees to carry every item between locations.
The operating principle depends on the conveyor configuration. Gravity roller conveyors use a slight incline to move products naturally, while powered roller conveyors use motors and mechanical drive components to maintain controlled movement.
Roller conveyors are particularly suitable for items with flat, stable bottom surfaces. Their performance depends on roller spacing, load distribution, product dimensions, and the condition of the conveyor structure.
Different Roller Conveyor Solutions for Industrial Applications
Selecting an appropriate conveyor configuration depends on the type of material being transported and the movement required within the facility.
Gravity Roller Conveyors
Gravity roller conveyors move products through natural gravitational force or manual pushing. They do not require a powered drive system, making them useful for straightforward material transfer.
Warehouses often use them for carton movement, packing stations, and short-distance transportation. Their simplicity can reduce mechanical complexity, although the conveyor requires suitable positioning and a controlled slope.
Powered Roller Conveyors
Powered roller conveyors use motors, drive belts, chains, or other transmission mechanisms to move products automatically. They are suitable for operations requiring consistent movement, controlled accumulation, and integration with automated handling equipment.
These systems can support production lines, distribution centers, and high-volume packaging operations. However, motor selection, load capacity, speed control, and maintenance access require careful consideration.
Accumulation Roller Conveyors
Accumulation conveyors allow products to collect temporarily without necessarily stopping the entire conveyor line. Depending on the design, individual sections can control product movement and maintain separation between items.
This arrangement helps coordinate different production stages when upstream and downstream processes operate at different speeds. Accumulation capability is particularly useful in packaging, sorting, and automated distribution environments.
Pallet Roller Conveyors
Pallet roller conveyors are designed to transport heavier unit loads supported by pallets. They generally use stronger frames, appropriately sized rollers, and drive arrangements suited to the expected load.
Manufacturing facilities and distribution centers use these systems to connect storage areas, loading points, and production processes. Correct pallet dimensions, weight distribution, and transfer requirements are essential when specifying equipment.
Important Components That Influence Conveyor Performance
A roller conveyor system contains several components that work together to support stable material movement.
The rollers provide the contact surface for transported products. Their diameter, material, spacing, and bearing arrangement influence load support, movement resistance, and suitability for different applications.
The conveyor frame supports the rollers and maintains structural alignment. It must accommodate operating loads, installation conditions, and the expected working environment.
Drive components are particularly important in powered systems. Motors, gearboxes, chains, belts, and control equipment determine how movement is transmitted and regulated.
Additional components may include:
Bearings: Support roller rotation and help reduce mechanical friction.
Side guides: Help maintain product alignment during transportation.
Sensors: Detect product positions and support automated control.
Transfer sections: Connect conveyor lines or change product direction.
Safety guards: Protect workers from accessible moving components.
Component selection should reflect actual operating conditions rather than relying only on general equipment specifications.
Where Roller Conveyor Systems Deliver Practical Value
Roller conveyor systems serve several industries because they can be configured for different material movement requirements.
In manufacturing facilities, they transport components between assembly stations, inspection areas, and packaging operations. This helps coordinate production activities and reduces unnecessary manual movement.
Warehouses use roller conveyors to transfer cartons, organize packing workflows, and connect storage operations with dispatch areas. Distribution centers may combine powered and gravity conveyors to support sorting and order preparation.
Packaging facilities use conveyor systems to move products through filling, sealing, labeling, and inspection stages. The equipment helps maintain a coordinated flow between individual processes.
Automotive and industrial manufacturing operations may use specialized roller conveyors for components, containers, and heavier assemblies. These applications require careful attention to load capacity, positioning accuracy, and mechanical durability.
How to Select the Right Roller Conveyor System
Choosing suitable equipment requires more than identifying the required conveyor length. Businesses should evaluate how products move through the facility and what operating conditions the equipment must handle.
Load characteristics are a primary consideration. Determine the maximum product weight, dimensions, bottom surface, and expected load distribution. Roller spacing must provide adequate support throughout transportation.
Movement requirements also influence the configuration. Gravity systems may be appropriate for simple transfer applications, while powered conveyors are more suitable when controlled speed and automated movement are necessary.
Facility layout should be evaluated before installation. Available floor space, elevation changes, transfer points, access routes, and connections with existing machinery can influence conveyor design.
Operating environment matters as well. Dust, moisture, temperature variations, cleaning procedures, and exposure to chemicals may affect the required frame materials, rollers, bearings, and protective components.
When comparing roller conveyor manufacturers and suppliers, evaluate their engineering capabilities, customization options, technical documentation, installation support, spare-parts availability, and maintenance services.
A supplier should be able to explain how the proposed configuration addresses the facility's actual load and workflow requirements. Detailed specifications are more useful than selecting equipment based on general capacity claims.
Maintenance and Safety Considerations
Regular maintenance helps maintain conveyor reliability and identify developing mechanical problems before they interrupt operations.
Inspect rollers for damage, unusual noise, restricted rotation, and excessive wear. Check bearings, drive chains, belts, fasteners, and supporting frames according to the manufacturer's maintenance instructions.
Powered systems also require inspection of motors, electrical connections, sensors, and control equipment. Unexpected changes in operating speed or product movement may indicate mechanical or control-related problems.
Safety requires equal attention. Accessible pinch points, moving rollers, drive mechanisms, and transfer areas should receive appropriate guarding. Emergency stops and isolation procedures should be provided where required by the equipment design and applicable workplace regulations.
Employees should receive training on safe operation, routine inspections, and procedures for reporting equipment problems. Maintenance should follow appropriate lockout and energy-isolation practices.
Frequently Asked Questions
What materials can roller conveyor systems transport?
They commonly transport cartons, containers, boxes, pallets, and other products with suitable supporting surfaces. The specific load capacity depends on roller dimensions, spacing, frame construction, and conveyor design.
What is the difference between gravity and powered roller conveyors?
Gravity conveyors move products through an incline or manual force, whereas powered conveyors use mechanical drive systems to control product movement. The appropriate option depends on distance, workflow, load requirements, and automation needs.
How do businesses determine roller conveyor capacity?
Capacity depends on product weight, dimensions, load distribution, roller specifications, frame strength, and operating conditions. Manufacturers should evaluate these factors before recommending a configuration.
Can roller conveyor systems integrate with automated warehouse equipment?
Yes. Suitable configurations can connect with sorting equipment, automated storage systems, sensors, pallet handling equipment, and other conveyor sections. Integration requires compatible controls, dimensions, transfer arrangements, and operating speeds.
What should businesses evaluate when choosing a roller conveyor manufacturer?
Consider engineering expertise, equipment specifications, customization capabilities, installation support, maintenance services, component availability, and experience with comparable industrial applications.
Conclusion
Roller conveyor systems provide a practical way to organize material movement across manufacturing facilities, warehouses, packaging operations, and distribution centers. Their effectiveness depends on selecting the right conveyor type, components, load capacity, and configuration.
Businesses should evaluate their operational requirements, facility layout, maintenance capabilities, and supplier support before selecting equipment. A properly specified roller conveyor system can support smoother workflows, more consistent material handling, and better coordination between industrial processes.
Related Post...
High-Volume Industrial PCB Assembly Plants: Discover Automated Assembly Processes
Updated: October 06, 2026
Read More
International Shipping Container Logistics Explore Smarter Cargo Coordination
Updated: October 19, 2026
Read More