Exploring Vision Inspection: Automation & Tech Guide
Vision inspection technology has become an important part of modern manufacturing, automation, and quality control processes.
Businesses across industries use vision inspection systems to identify defects, verify product quality, and improve production consistency.
Unlike manual inspection methods, vision inspection uses cameras, lighting systems, sensors, and intelligent image processing technologies to evaluate products automatically. These systems can operate continuously and provide highly accurate inspection results in fast-moving production environments.
As Industry 4.0 and smart manufacturing continue to evolve, vision inspection systems play a critical role in helping organizations improve efficiency, reduce errors, and maintain product standards.
Quick Facts About Vision Inspection
| Feature | Details |
|---|---|
| Primary Function | Automated Quality Inspection |
| Core Technology | Cameras and Image Processing |
| Inspection Speed | Real-Time Operation |
| Common Industries | Manufacturing, Electronics, Automotive |
| Detection Capabilities | Defects, Measurements, Verification |
| Automation Support | High |
| Data Collection | Continuous Monitoring |
| Integration | Production Line Systems |
What Is Vision Inspection?
Vision inspection is an automated process that uses cameras and imaging technology to analyze products, components, or materials. The system captures images and evaluates them against predefined standards.
The goal is to identify defects, verify dimensions, confirm assembly accuracy, and ensure product consistency.
For example, a beverage packaging facility may use vision inspection systems to verify label placement, cap alignment, and barcode readability before products leave the production line.
Understanding the Concept of Vision Inspection
Vision inspection combines optical imaging with automated analysis. Cameras capture images while processing systems evaluate those images using programmed inspection criteria.
Unlike human inspection, automated vision systems can inspect thousands of products per hour with consistent accuracy.
Why Vision Inspection Matters
- Improves product quality
- Supports manufacturing automation
- Reduces inspection errors
- Enhances traceability
- Increases production efficiency
- Provides real-time monitoring
Key Statistics and Industry Facts
| Metric | Industry Insight |
|---|---|
| Inspection Method | Automated image-based evaluation |
| Production Usage | Widely used in automated manufacturing |
| Detection Capability | Surface defects, dimensions, assembly verification |
| Operational Mode | Continuous real-time inspection |
| Data Collection | Supports production analytics |
| Industry Adoption | Growing with Industry 4.0 initiatives |
Vision Inspection System Architecture
A vision inspection system consists of several interconnected components working together to capture, process, and evaluate images.
Image Acquisition Layer
This layer captures images using industrial cameras positioned at specific inspection points.
Lighting System
Proper lighting ensures consistent image quality. Different lighting methods highlight different product features.
Image Processing Unit
The processing system analyzes captured images and compares them with inspection criteria.
Decision Engine
The decision engine determines whether a product passes or fails inspection.
Communication Interface
Inspection results are transmitted to manufacturing systems, databases, or control platforms.
Data Storage Layer
Inspection records support traceability and quality analysis.
Main Components of Vision Inspection Systems
| Component | Function |
|---|---|
| Industrial Camera | Captures images |
| Lens System | Focuses image details |
| Lighting Equipment | Improves image clarity |
| Processing Unit | Analyzes images |
| Inspection Algorithms | Evaluates quality |
| Communication Module | Transfers inspection results |
| Storage System | Maintains records |
| Control Interface | Manages operations |
Types of Vision Inspection Systems
2D Vision Inspection
2D systems evaluate flat images and are commonly used for identification and defect detection.
Common Applications
- Barcode verification
- Label inspection
- Surface defect detection
- Character recognition
3D Vision Inspection
3D systems capture depth information and analyze object dimensions.
Common Applications
- Dimensional measurement
- Assembly verification
- Shape analysis
- Robotics guidance
Smart Camera Systems
These systems combine imaging and processing within a single device.
Advantages
- Compact design
- Simplified installation
- Faster deployment
AI-Based Vision Inspection
Artificial intelligence enhances inspection capabilities by identifying complex patterns and anomalies.
Advantages
- Adaptive learning
- Advanced defect recognition
- Improved accuracy
Vision Inspection Technology Comparison
| Technology | Inspection Capability | Typical Applications |
|---|---|---|
| 2D Vision | Surface Inspection | Labels, Packaging |
| 3D Vision | Dimensional Analysis | Assembly Verification |
| Smart Cameras | Compact Inspection | Production Cells |
| AI Vision | Complex Pattern Detection | Advanced Manufacturing |
How Vision Inspection Works
Step 1: Product Positioning
The product enters the inspection area.
Step 2: Image Capture
Industrial cameras capture images of the product.
Step 3: Lighting Optimization
Lighting systems highlight features for analysis.
Step 4: Image Processing
Software analyzes captured images.
Step 5: Quality Evaluation
The system compares results with inspection criteria.
Step 6: Decision Making
Products are classified as acceptable or defective.
Step 7: Data Recording
Inspection results are stored for future analysis.
Vision Inspection Workflow Table
| Stage | Function |
|---|---|
| Product Entry | Positioning |
| Image Capture | Photography |
| Lighting Control | Feature Enhancement |
| Processing | Data Analysis |
| Evaluation | Quality Verification |
| Decision | Pass/Fail Classification |
| Recording | Data Storage |
Technical Specifications Explained
Camera Resolution
Higher resolution provides more image detail.
| Resolution Category | Typical Usage |
|---|---|
| Standard Resolution | Basic Inspection |
| Medium Resolution | General Manufacturing |
| High Resolution | Precision Inspection |
| Ultra High Resolution | Semiconductor Applications |
Frame Rate
Frame rate determines how many images are captured each second.
Field of View
The field of view defines the inspection area.
Accuracy
Accuracy measures how precisely the system identifies features and defects.
Processing Speed
Fast processing supports high-speed production environments.
Benefits and Advantages
Improved Product Quality
Vision inspection helps identify defects before products move to the next production stage.
Increased Efficiency
Automated inspection reduces manual evaluation requirements.
Consistent Inspection
Inspection criteria remain consistent across production shifts.
Real-Time Monitoring
Issues can be detected immediately during production.
Better Traceability
Inspection data supports quality documentation and reporting.
Reduced Production Errors
Automated analysis minimizes variability in inspection results.
Real-World Applications
Automotive Manufacturing
Vision systems inspect components, assemblies, and markings.
Electronics Production
Inspection verifies circuit boards and component placement.
Pharmaceutical Manufacturing
Packaging verification and labeling inspection are common applications.
Food and Beverage Production
Systems inspect packaging integrity and product labeling.
Aerospace Manufacturing
Precision inspection supports quality and compliance requirements.
Packaging Industry
Vision systems verify print quality and package consistency.
Industry Applications Table
| Industry | Common Application |
|---|---|
| Automotive | Component Inspection |
| Electronics | PCB Verification |
| Food Processing | Packaging Inspection |
| Pharmaceutical | Label Verification |
| Aerospace | Precision Measurement |
| Packaging | Print Quality Inspection |
Material and Product Inspection Matrix
| Inspection Target | Vision Inspection Capability |
|---|---|
| Labels | Excellent |
| Barcodes | Excellent |
| Electronics | Excellent |
| Metal Components | Excellent |
| Plastic Parts | Excellent |
| Glass Products | Good |
| Packaging Materials | Excellent |
| Medical Devices | Excellent |
Common Challenges and Solutions
| Challenge | Solution |
|---|---|
| Lighting Variations | Controlled Lighting Systems |
| Product Position Changes | Positioning Fixtures |
| Reflection Issues | Specialized Illumination |
| High Production Speed | Faster Cameras |
| Complex Defects | AI-Based Analysis |
| Data Volume | Advanced Storage Systems |
Environmental Considerations
Vision inspection contributes to sustainable manufacturing practices by improving quality and reducing unnecessary waste.
Reduced Material Waste
Early defect detection helps reduce rejected products.
Improved Resource Efficiency
Consistent inspection minimizes rework requirements.
Data-Driven Manufacturing
Inspection data supports process optimization.
Lower Production Losses
Real-time detection prevents large-scale quality issues.
Industry Standards and Safety
Vision inspection systems often operate within manufacturing quality frameworks and industrial automation standards.
Quality Assurance Requirements
Inspection systems support quality management processes.
Equipment Safety
Industrial cameras and lighting systems must comply with workplace safety requirements.
Data Integrity
Inspection records should be securely maintained.
System Validation
Performance validation ensures inspection reliability.
Maintenance Schedule
| Maintenance Task | Frequency |
|---|---|
| Camera Cleaning | Weekly |
| Lens Inspection | Weekly |
| Lighting Verification | Monthly |
| Calibration Check | Monthly |
| System Backup | Monthly |
| Performance Validation | Quarterly |
| Hardware Inspection | Quarterly |
Best Practices for Vision Inspection
Maintain Consistent Lighting
Stable illumination improves image quality.
Perform Regular Calibration
Calibration helps maintain inspection accuracy.
Monitor System Performance
Continuous monitoring identifies performance changes.
Maintain Clean Optics
Clean lenses support image clarity.
Validate Inspection Criteria
Inspection parameters should be reviewed periodically.
Secure Inspection Data
Data retention supports traceability and analysis.
Expert Insights
Vision inspection systems are most effective when integrated into a broader manufacturing automation strategy. High-quality cameras alone do not guarantee reliable inspection results. Lighting design, lens selection, positioning accuracy, image processing algorithms, and system calibration all contribute to overall performance.
Manufacturers increasingly combine machine vision with artificial intelligence to improve defect detection capabilities. AI-driven systems can identify subtle variations that traditional rule-based inspection methods may miss, making them valuable for complex manufacturing environments.
Future Trends and Industry Insights
Artificial Intelligence Integration
AI continues to expand inspection capabilities.
Edge Computing
Processing images closer to production equipment reduces latency.
Smart Factory Connectivity
Vision systems increasingly connect with Industry 4.0 platforms.
Advanced 3D Inspection
More industries are adopting three-dimensional inspection methods.
Predictive Quality Analytics
Inspection data helps identify process trends before defects occur.
Robotics Integration
Machine vision supports automated robotic guidance and inspection.
Frequently Asked Questions
What is vision inspection?
Vision inspection is an automated process that uses cameras and image analysis technology to evaluate products and identify defects.
How does vision inspection improve quality?
It provides consistent and repeatable inspections that help identify defects during production.
What industries use vision inspection?
Automotive, electronics, aerospace, pharmaceutical, packaging, and food processing industries commonly use vision inspection.
What is the difference between 2D and 3D vision inspection?
2D inspection analyzes flat images, while 3D inspection evaluates depth and dimensional information.
Why is lighting important in vision inspection?
Lighting improves image quality and helps highlight product features for accurate analysis.
Can vision inspection detect surface defects?
Yes, it is commonly used to identify scratches, dents, cracks, and other surface imperfections.
What role does AI play in vision inspection?
AI improves defect detection by recognizing complex patterns and anomalies.
What is a smart camera system?
A smart camera combines imaging and processing capabilities within a single device.
How does vision inspection support automation?
It provides automated quality verification without manual inspection.
What factors affect inspection accuracy?
Camera quality, lighting, calibration, positioning, and image processing algorithms all influence accuracy.
How often should systems be calibrated?
Calibration schedules vary by application, but regular verification helps maintain reliable performance.
Can vision inspection collect production data?
Yes, inspection systems often record quality data for analysis and traceability.
What is machine vision?
Machine vision is the broader technology field that includes automated image capture and analysis systems.
Is vision inspection suitable for high-speed production?
Yes, modern systems are designed for real-time operation in fast-moving manufacturing environments.
What future developments are expected?
AI integration, advanced analytics, edge computing, and smart factory connectivity are expected to drive future growth.
Conclusion
Vision inspection technology has become a cornerstone of modern automation and quality control. By combining industrial cameras, intelligent image processing, advanced lighting systems, and automated decision-making, these systems help manufacturers improve product quality, efficiency, and consistency.
As smart manufacturing continues to evolve, vision inspection will play an even greater role in supporting Industry 4.0 initiatives, predictive quality management, and automated production environments. Organizations that understand and implement vision inspection technologies effectively can benefit from improved operational performance and enhanced quality assurance.
Related Post...
Wafer Processing Equipment Insights: Semiconductor Manufacturing
Updated: September 21, 2026
Read More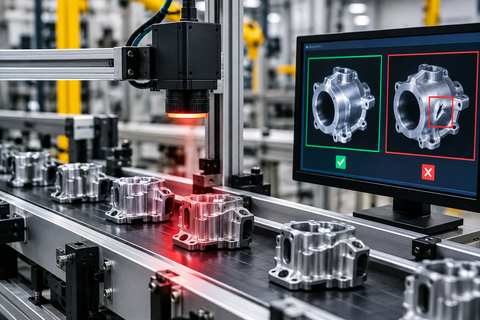
Defect Detection: Complete Guide to Inspection Technologies and Quality Control
Updated: September 21, 2026
Read More